A standard mould base can reduce lead time and cost, but it does not replace cavity, cooling, ejection and transfer-to-series analysis.
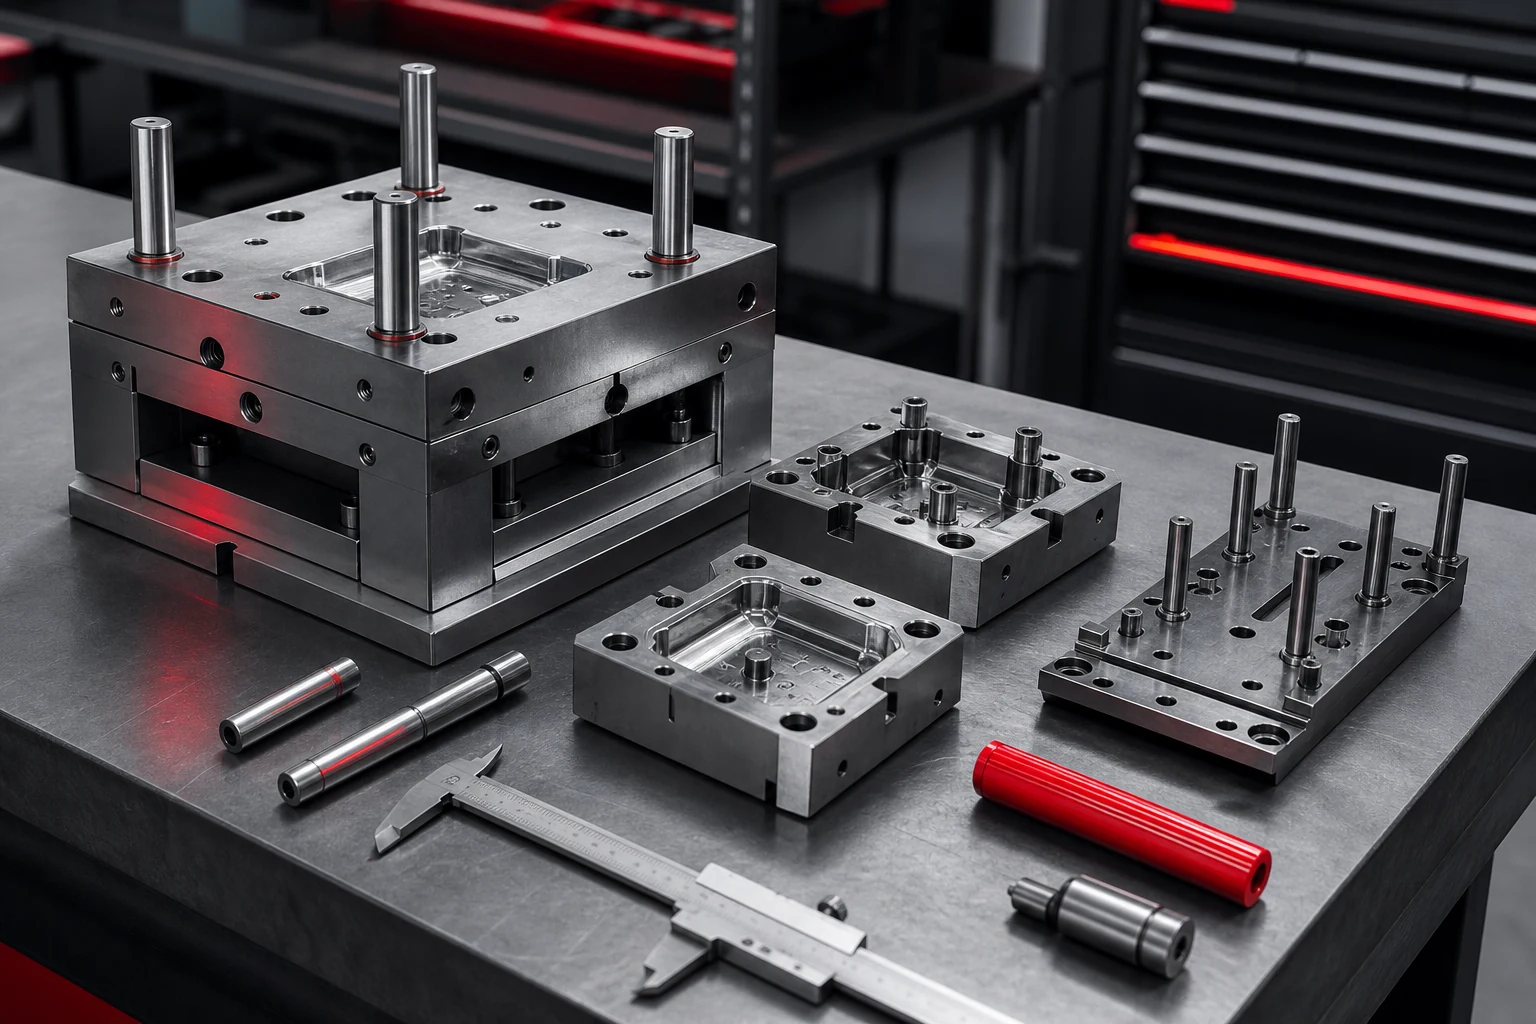
Key idea: a standard mould base removes repetitive work, but the industrial decision depends on cavity, flow, cooling, ejection and dimensional control.
What a standard mould base actually standardises
A standard mould base provides a proven mechanical architecture: plates, guiding, ejector accommodation and components available on predictable lead times. In a prototype project, it can focus effort on what defines the part: inserts, cavity, feeding and shut-off areas.
That saving does not make the mould generic. The part still sets its own requirements for size, tolerance, material, finish, number of cavities and test volume. The base may be reusable; the evidence the prototype must generate is not.
When it genuinely accelerates the project
A standard option is appropriate when the part envelope fits available formats and validation needs to iterate geometry or inserts without rebuilding the whole assembly. It also helps when the goal is to learn early about filling, shrinkage, ejection or appearance with production material before committing to series tooling.
For the time saving to be real, the project should define which components remain fixed and which elements can change. An available base does not offset a cavity that forces cooling, guidance or ejection to be rebuilt every time a critical dimension changes.
What remains part-specific
The cavity and insert define geometry; the gate and runner arrangement affect flow path, pressure and orientation; and ejection must support the part without distortion or marks. Cooling must respond to wall thickness, local masses, cosmetic zones and functional tolerances, not base size alone.
Venting, fine shut-offs, maintenance access and assembly stiffness also require review. When a standard solution creates a compromise in any of these areas, the expected saving can reappear as rework, machine adjustments or uncertainty during transfer to production.
What the prototype must validate
The question is not whether one first part can be produced, but whether the process has margin. The trial should combine defect observation with repeated measurement to understand what happens when material, temperature, pressure or cycle time change slightly.
- Filling and pressure: confirm that remote areas and section changes complete without operating at a machine extreme.
- Ejection: check for marks, ejection distortion and stability of thin-wall or flexible features.
- Cooling and shrinkage: measure functional dimensions after a defined stabilisation period, not only at ejection.
- Appearance: review weld lines, gloss, gate vestige and cosmetic surfaces using the final material.
- Repeatability: compare several parts and vary parameters within a reasonable range to identify the process window.
Signals that a standard base is not enough
A standard base stops being efficient when the part requires cooling very close to the cavity, complex side actions, high ejection loads, especially tight tolerances or an envelope that compromises stiffness and access. In those cases, a larger base, a semi-standard architecture or a purpose-designed solution may be better.
The comparison should include the cost of learning too late. If the prototype does not reproduce the conditions governing warpage, ejection, filling or dimensional variation, it only moves risk into production tooling. Validating early supports evidence-based choices and reduces uncertainty; it does not suggest that a standard component alone resolves industrialisation.
Frequently asked questions about standard mould bases
Does a standard mould base work for any part?
No. It accelerates common architecture, but feasibility depends on size, geometry, ejection, cooling, feeding and material.
Which parts remain project-specific?
The cavity, insert, feeding strategy, ejection, venting and validation criteria remain specific to each part.
Why does it help P2P?
It concentrates lead time and cost on what changes in each project: the validated geometry and the learning transferred to production tooling.